Jam and Sauce Filling Line
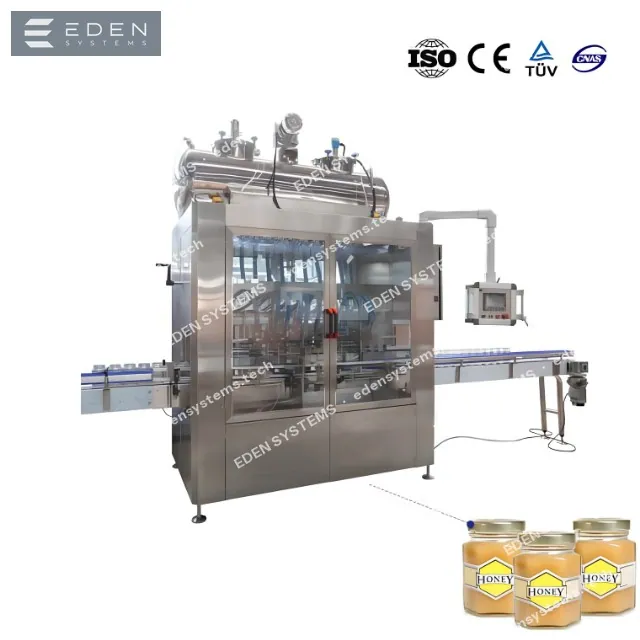
A rotary line for jams, preserves, sauces, honey and pastes: piston dosing of hot product, vacuum twist-off capping and jar cooling.
- Product
- Jams, preserves, ketchup, sauces, honey, nut butters
- Viscosity
- up to 50,000 cP, particulates up to 10 mm
- Container
- Glass and PET, 0.1–1.0 L, neck 38–82 mm
- Output
- 1,000–8,000 jph
- Dosing
- Piston, servo-driven, ±0.5 %
- Product temperature
- 80–90 °C
- Capping
- Twist-off with vacuuming, 4–8 heads
- Materials
- AISI 316L, jacketed hopper with agitator
Line parameters
About the solution
Viscous products with fruit pieces cannot be gravity-filled. Dosing is performed by servo-driven piston cylinders: volume is set by piston stroke, speed by the servo-motor profile, and a shut-off valve prevents stringing and dripping at the neck.
Product is fed hot (80–90 °C) from the cooking kettle through a jacketed hopper with an agitator. After twist-off capping, the jar is inverted to sanitize the lid, cooled in a tunnel and moves on to labeling.
Built into the design
Servo-piston doser
Speed profile is tuned to the product: slow start against splashing, fast fill, gentle cut-off.
Jacketed hopper
Heating and agitation keep the product homogeneous and flowable throughout the shift.
Vacuum capping
The lid is applied in a steam or vacuum environment — on cooling, a control vacuum forms.
Cleaning without disassembly
A CIP circuit washes the doser and hopper with hot solution; removable parts strip down without tools.
Line composition along the product flow
8 positions along the product flow. Every unit opens in the catalog: series, specifications, scope of supply and a quote request.
- 1
1. Jar feeding and rinsing
Container depalletizing, air blow-off or rinsing with drying.
Sauce and thick-product filling →
- 2
2. Cooking area and hopper
Feeding product from the kettle into a jacketed, agitated, heated hopper.
Sauce and thick-product filling →
- 3
3. Piston doser
Rotary or in-line dosing of a metered volume at 80–90 °C.
Sauce and thick-product filling →
- 4
4. Twist-off capping
Lid feeding, vacuuming and screw application with torque control.
Capping equipment →
- 5
5. Inverter and cooling
Tilting the jar to sanitize the lid and a stepped cooling tunnel.
Sauce and thick-product filling →
- 6
6. Inspection
Weight, fill-level and lid-vacuum checks, rejection.
Marking and quality inspection →
- 7
7. Labeling and date coding
Pressure-sensitive label, back label and batch date coding.
Labelling equipment →
- 8
8. Case packing and palletizing
Case former, packing, sealing and palletizing.
Packing and palletising →
Line model selection
Selecting a hot-fill rotary tri-block
Contact volumetric (piston) dosing method, round containers, vacuum drip suction after filling prevents dripping.
| Rinsers / valves / capping heads | Output (0.5 L) | Container |
|---|---|---|
| 12 / 12 / 4 | 2,000–3,000 btl/h | Glass / PET, 100–1,000 mL |
| 18 / 18 / 6 | 3,500–5,000 btl/h | Glass / PET, 100–1,000 mL |
| 24 / 24 / 8 | 5,000–7,000 btl/h | Glass / PET, 100–1,000 mL |
| 32 / 32 / 10 | 7,000–9,000 btl/h | Glass / PET, 100–1,000 mL |
Output is given for a sauce with viscosity up to 2,000 cP at a fill temperature of 80–90 °C; for chunky jams, cycle time increases by 10–20%.
Containers and packaging
| Container type | Volume | Closure | Packaging |
|---|---|---|---|
| Glass jar | 100–1,000 mL | Twist-off, metal | Corrugated case with dividers |
| PET bottle | 150–750 mL | Plastic cap | Shrink film or case |
Operating conditions: 10–40 °C, no condensation. Power supply 380 V ±5%, 3-phase, 50 Hz ±1%.
Line process flow
Hot filling of jams and sauces is built around a single rotary triblock, but the line's "head" and "tail" differ depending on the container: PET needs a blow molder and air conveyor, while glass needs a jar unscrambler and case packer.
Key features of hot filling
- Round containers, contact volumetric (piston) dosing method
- Vacuum suck-back after filling — eliminates drips and stringing at the neck
- Frame and top plate made of AISI 304 stainless steel
- Contact parts and product tank — polished with no dead zones
- Interface for connection to the customer's aseptic circuit
- Core components and the touch panel are branded, industrial-grade PLC
Layout for sauces and ketchups in plastic containers with in-line preform blow molding.
- 1Water treatment
- 2Sauce cooking and blending unit
- 3Blow molder or bottle unscrambler
- 4Air conveyor + slat conveyor
- 53-in-1 rotary triblock (rinse — fill — cap)
- 6Light inspection station
- 7Cooling tunnel with shower
- 8Labeling machine
- 9Coder / batch marking
Key line stations
What sits behind the nameplate output: contact-part execution, operating logic and service points for every station.
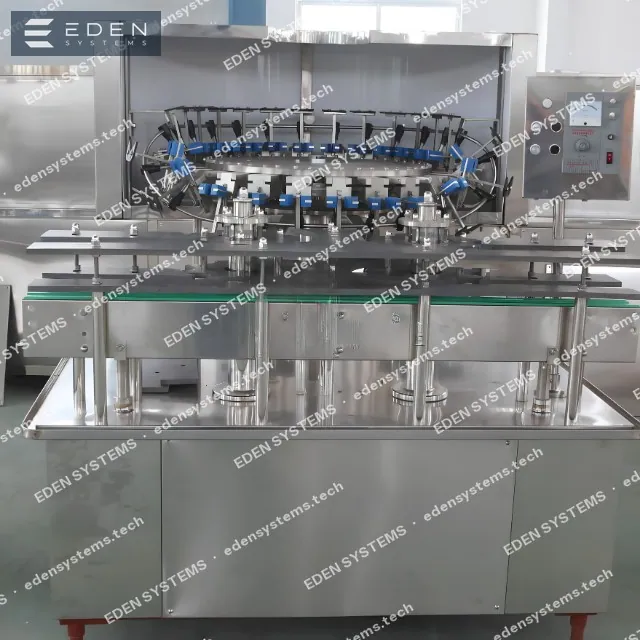
Rinsing heads
Container preparation
- AISI 304/316 stainless nozzles and manifold with fan-jet spray: lower water consumption and more even rinsing over the entire inner surface.
- Neck-grip gripper with a polymer insert holds the bottle by the finish, minimizing the risk of preform crushing or scratching.
- Rinsing pump and piping in sanitary design, the circuit disassembles without tools.
- Rinse-water recirculation with filtration — up to 30% savings compared to drain discharge.
Core machines of the line
Equipment of the “Jam and Sauce Filling Line” layout: each tile opens the catalog with series, specifications and a quote request for that machine.
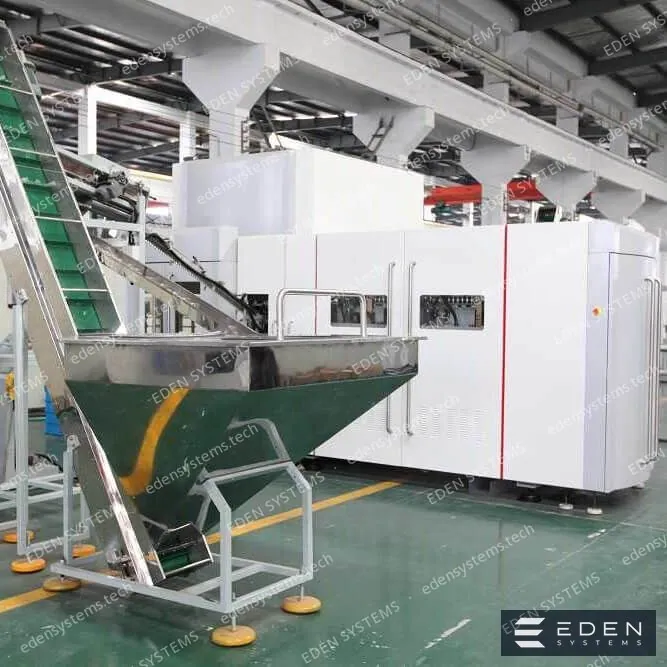
Jar unscrambler / blow molder
Container infeed to the line: an unscrambler places glass jars on the conveyor, while a preform blow molder handles PET.
Air and slat conveyor
Air conveyance for lightweight PET containers by the neck ring, and a chain conveyor with lubrication and anti-tip guides for heavy glass jars.
Rotary 3-in-1 triblock
Rinsing, piston hot filling at 80–90 °C, and twist-off capping on a single frame with no intermediate transfer.
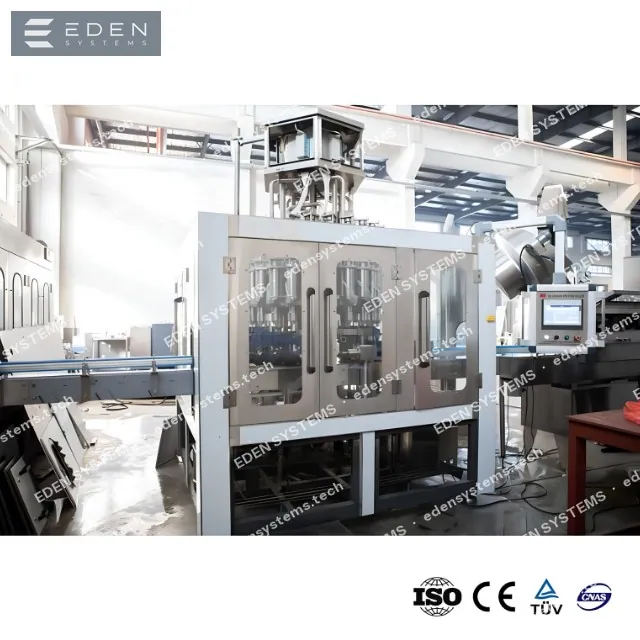
Piston doser for viscous products
Contact volumetric dosing with a diving nozzle and vacuum drip suck-back, flow passage sized for particles up to 10 mm.
Light inspection station
Checks fill level, foreign inclusions and cap integrity against a light source before cooling.
Cooling tunnel (shower type)
Step-down cooling of jars after hot filling: stainless steel housing, evenly spaced nozzles, hinged top for maintenance.
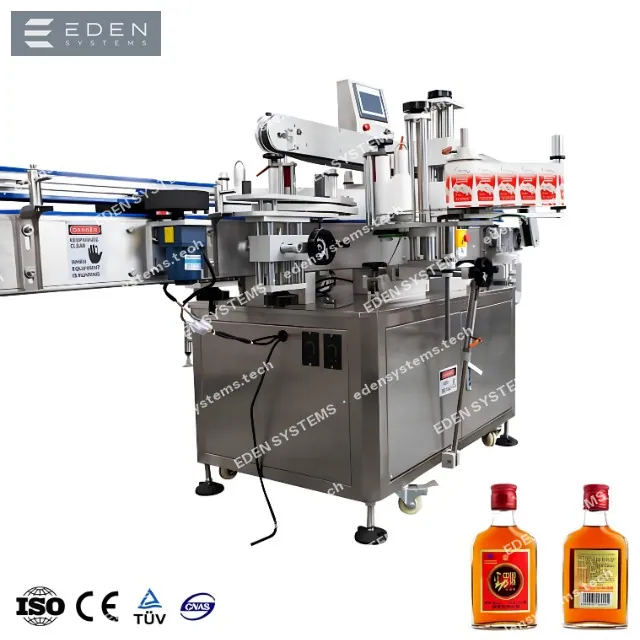
Labeling machine
Self-adhesive body and back label; for PET — heat-shrink sleeve or hot-melt OPP label.
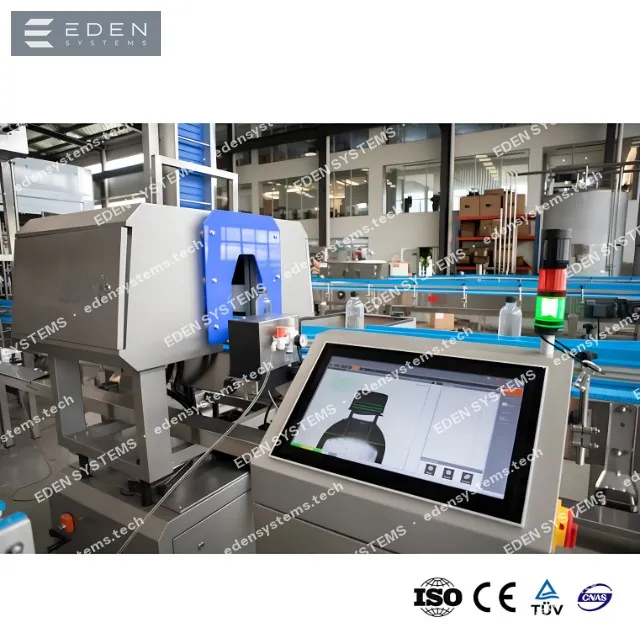
Coder and batch marking
Prints the filling date, shift number and expiration date with a code legibility check.
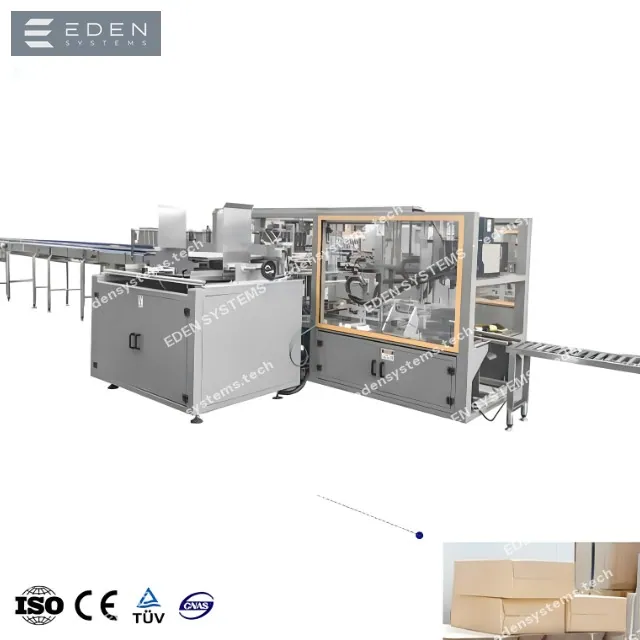
Case packing and palletizing
Loads jars into corrugated cases with dividers, seals the case, and forms the pallet layer by layer.
Which closure do you use
The cap type defines the capping block: heads, feeding and orientation of the closure, torque or press-on force. State your option in the request and we will select the head and sorter for it.
TO-53 … TO-82
Metal twist-off lid
For jars with sauces, jams and preserves. Works together with vacuum or steam injection before capping.
Capping unit: Seaming/screwing head
24 mm, 28 mm
Flip-top / disc-top cap
The closed cap is fed pre-oriented to the label so the flap faces the right direction after capping.
Capping unit: Press head + tightening
foil 0.2–0.9 mm
Induction liner under the cap
The liner is welded to the finish after capping — tamper protection and seal integrity during transport.
Capping unit: In-line induction sealer
Auxiliary systems of the line
The engineering utilities without which a line never reaches its rated output: water and product preparation, sanitation, container handling.
Cooking and blending block
Preparing jam, sauce or paste.
- Vacuum evaporator or a jacketed kettle with an agitator
- Mass-based sugar, pectin and acid dosing, recipe stored in the controller
- Product deaeration — color and flavor preserved, no headspace bubble in the jar
- Heated buffer tank with a slow agitator
Viscous-product dosing
High-viscosity product with particulates.
- Piston doser with a flow path clearing particulates up to 10 mm
- Drip-free lifting nozzle with a heated tip
- Heated jacket on the product tank and lines
- Dose accuracy ±0.5%, weight-checked at a sampling station
Pasteurization and container cooling
Sterilizing the packed product.
- Tunnel pasteurizer or an autoclave, depending on the recipe
- Stepped shower cooling, protecting glass from thermal breakage
- Process lethality monitored via a control container
- Air blow and drying before labeling
CIP station (clean-in-place)
Hot-solution wash of the viscous path with turbulent flow.
- Alkali, acid and hot-water tanks holding temperature within ±2 °C
- Recipe-driven wash programs: phase time, concentration and flow are logged
- Flow meter on the supply line — actual flow is verified, not assumed from the nameplate
- Filtered detergent return to the tanks; discharge only once the solution is spent
Coding and inspection
Date, batch and best-before date on the cap or label.
- Inkjet or laser coder: date, shift, batch number, traceability code
- Fill-level, cap presence and seating inspection with automatic reject to a pocket
- Good/reject product counters logged per shift hour
- Ready for mandatory marking: case and pallet aggregation at the line outfeed
Packing and palletizing
Case with dividers, palletizing and wrapping.
- Shrink film pack or corrugated case, format tailored to the retailer's requirements
- Layer palletizer to a defined pattern, robotic version for constrained floor space
- Pallet wrapper with pre-stretch film: lower film consumption, pallet withstands transport
- SSCC pallet label printing and application, data handoff to the ERP system
FAQ
How to choose between a rotary and an in-line doser?
Below about 2,000 jars per hour an in-line doser is more economical: cheaper and simpler to maintain. Above that, only a rotary doser keeps up — the in-line design runs out of cycle time.
How is varying viscosity handled?
The servo drive lets you store a separate speed profile for each recipe and switch by selecting the recipe on the operator panel.
How much does the Jam and Sauce Filling Line cost?
Price on request: the budget depends on output, container type, line composition and the level of automation. After a short brief we send a preliminary estimate within 1–2 working days and a full quotation broken down by machine within 3–5 days.
What are the delivery and commissioning lead times?
Standard machines ship 8–12 weeks after the specification is confirmed, complete lines 12–20 weeks. Transport takes 2–6 weeks depending on the route; installation and commissioning on site take 2–4 weeks, with operator training included.
What output does this line reach?
The working range is 1,000–8,000 jph. Exact output is confirmed against your container, product and shift plan: we calculate the line balance and keep a margin on the bottleneck machine.
Request a quote: Jam and Sauce Filling Line
Tell us the product, the container and the target output — we will return the line composition, a layout, a budget range and a delivery schedule.
Related solutions
Lines with a similar equipment set — useful when you plan several products on one site.
1,000–20,000 bph
Vegetable Oil Filling Line
Weight or volumetric oil filling into PET, glass and tinplate with capping, induction sealing, labelling and case packing.
Open solution2,000–36,000 bph
Drinking Water Filling Line, 0.33–1 L
Rinser-filler-capper monobloc for PET, water treatment, labelling and shrink packing.
Open solution2,000–24,000 bph
Beer Bottling Line (Glass)
Isobaric filling with low TPO, crown capping and tunnel pasteurization.
Open solutionServices for this line
Engineering, logistics, installation and service that turn this line into a working production site.
Digital layer
Any line can be supplied with a digital layer
SCADA, MES, OEE monitoring, batch traceability and integration with plant systems — engineered together with the line, not bolted on later.